Confirm the on-site generation and accepted gas boundary
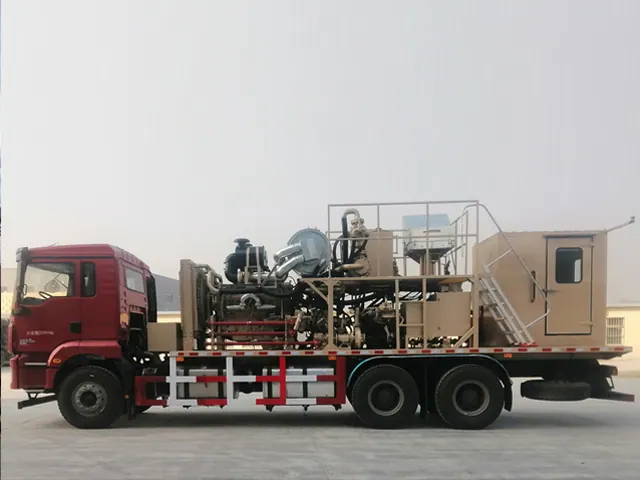
This nitrogen generation truck uses an expressly selected prepared-air and separation arrangement. PSA and membrane systems need their own configuration-specific response; they are not liquid-nitrogen pumping and vaporization equipment. Identify actual air compression, treatment, generation, drive and any booster or buffer. Accept gas quality, usable flow, delivery pressure and duration together at a defined boundary and stated site conditions.
Separate maximum ratings do not establish simultaneous capability. High-pressure boosting, independent standby, external distribution and destination acceptance require explicit scope and evidence. Nitrogen is not breathing air and can create an oxygen-deficient atmosphere. Keep actual operation, maintenance and gas release under competent personnel, configuration-specific manufacturer information and approved project procedures.
Use condition-based checks around a fixed maintenance schedule
The nitrogen generation truck works in a demanding combination of vibration, dust, weather, transport loads and intermittent high duty. Preventive maintenance should combine calendar intervals, operating hours, job cycles and condition trends. The objective is not simply to replace parts; it is to detect changes before they affect producing a continuous on-site nitrogen supply for purging, inerting, pressure support and oilfield service.
Start with the manufacturer manual and component instructions, then adapt intervals using actual service severity. Record pressure, temperature, vibration, oil condition, leakage and alarm history consistently so changes can be compared between jobs.
Practical inspection schedule
| Interval | Typical work | Control point |
|---|---|---|
| Pre-assignment review | Equipment-specific tasks and identified open defects | Approved readiness basis |
| Post-assignment review | Recorded duty, quality and relevant observations | Accepted handover record |
| Scheduled service | Actual component work and intervals | Manufacturer information and service history |
| Condition investigation | Relevant feed-air, instrument and performance evidence | Qualified provider assessment |
| Major work | Approved return-to-service scope | Configuration-specific verification |
Troubleshooting by symptom, not guesswork
| Symptom | Possible causes | First disciplined action |
|---|---|---|
| Accepted flow below target | Feed conditions, controls, measurement or equipment condition | Collect actual duty and instrument evidence for qualified review |
| Unaccepted gas quality | Sample, feed-air, separation or control condition | Use approved quality-release and investigation arrangements |
| Abnormal temperature or vibration | Actual installed equipment and service history | Follow manufacturer and site response requirements |
| Repeated alarm or trip | Actual process event or measurement and control issue | Do not bypass protection; retain evidence for qualified assessment |
Use manufacturer-supported investigation and approved project procedures with competent personnel. Verify the evidence before assigning a cause; do not bypass protection or infer a generic adjustment from a symptom.
Build a critical-spares list from failure consequence
Stock parts that combine meaningful failure probability with long delivery time or high downtime impact. For this package, start with service kits for air compressor package, membrane or PSA separation system, identified gas-treatment arrangement, nitrogen analyzer and control panel. Include seals, filters, sensors, relays, approved lubricants and the special tools needed to install them correctly.
- Identify every spare by manufacturer, model and drawing reference
- Separate commissioning, two-year operating and overhaul spares
- Store elastomers, electronics and lubricants within shelf-life limits
- Preserve large rotating or pressure components during storage
- Update inventory after every withdrawal and configuration change
Maintenance records that protect lifecycle value
Keep a history for each unit: serial numbers, job hours, operating envelope, inspections, alarms, repairs, parts fitted and calibration status. These records support warranty discussions and reveal whether repeated faults are caused by service severity, installation, operation or component selection.
After significant work, use an approved equipment-specific return-to-service plan with competent personnel. Retain installed references, relevant findings and gas-delivery verification, resolving open acceptance conditions before the next assignment.
Connect service decisions to the installed equipment
Review compressor and treatment condition, generation response, instruments and any booster together with the actual duty and feed-air history. A changed quality or flow indication can have several causes. Use the responsible manufacturer information to investigate and plan work rather than assume a universal service interval, separation-medium failure or control adjustment.
Retain accepted gas cases, final component references, relevant evidence and open deviations together. Review material changes to equipment, site conditions and external interfaces before relying on the prior response. Actual field work remains subject to approved equipment-specific and project arrangements.
For broader industry context, consult OSHA oil and gas extraction safety guidance. Project requirements and applicable codes must still be confirmed for the destination country and end user.
Frequently asked questions
How often should a nitrogen generation truck be serviced?
Use the manufacturer intervals, then adjust by operating hours, job cycles, environment and condition trends. Pre-job and post-job inspections remain essential.
What spare parts should be kept on site?
Prioritize seals, filters, sensors, service kits and other items with long lead time or high downtime consequence for the installed component models.