Confirm the on-site generation and accepted gas boundary
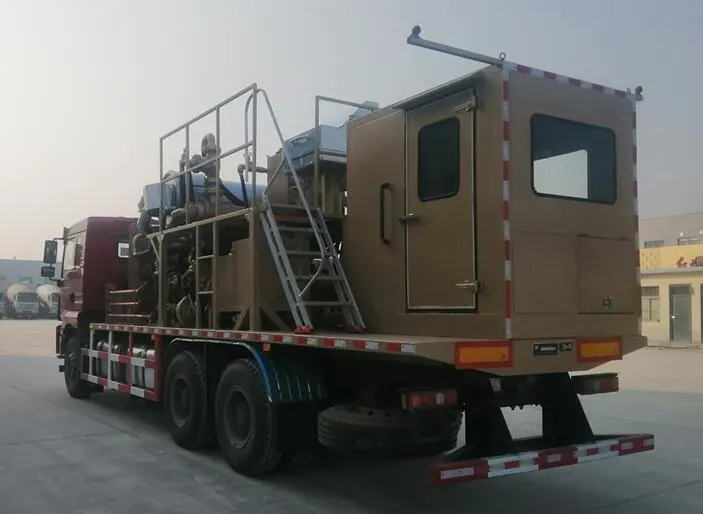
This nitrogen generation truck uses an expressly selected prepared-air and separation arrangement. PSA and membrane systems need their own configuration-specific response; they are not liquid-nitrogen pumping and vaporization equipment. Identify actual air compression, treatment, generation, drive and any booster or buffer. Accept gas quality, usable flow, delivery pressure and duration together at a defined boundary and stated site conditions.
Separate maximum ratings do not establish simultaneous capability. High-pressure boosting, independent standby, external distribution and destination acceptance require explicit scope and evidence. Nitrogen is not breathing air and can create an oxygen-deficient atmosphere. Keep actual operation, maintenance and gas release under competent personnel, configuration-specific manufacturer information and approved project procedures.
Start with the job decision
Nitrogen Generation Truck projects succeed when the equipment scope is tied to a defined operating duty: producing a continuous on-site nitrogen supply for purging, inerting, pressure support and oilfield service. A useful project document separates normal duty, maximum credible duty, standby or transient conditions and the physical interfaces available at site. This keeps procurement language connected to field reality.
Record nitrogen purity, standard flow capacity, delivery pressure and ambient conditions as ranges rather than isolated peak figures. The supplier can then explain how the air compressor package, membrane or PSA separation system, identified gas-treatment arrangement and nitrogen analyzer and control panel work together across the intended envelope.
Compare configurations by duty case, not brochure labels
Alternative packages may use different component sizes, control philosophies or levels of redundancy. Create separate evaluation cases for pipeline purging, tank inerting, underbalanced operations and nitrogen lift and pressure testing. Score whether each option meets the required range, not merely the maximum stated capacity.
| Review item | What to confirm | Evidence or input |
|---|---|---|
| air compressor package | Prepared-air capacity and supported conditions | Identified compressor and treatment response |
| membrane or PSA separation system | Quality-specific usable nitrogen output | Actual selected separation response |
| identified gas-treatment arrangement | Required feed or product condition at its boundary | Treatment and measurement scope |
| nitrogen analyzer and control panel | Quality indication and accepted release functions | Instrument and functional evidence |
Include logistics and maintainability in the decision
Review transport envelope, setup time, crew requirements, consumables, routine service access and critical-spares lead times. A configuration with a modestly higher purchase price can be the better project choice when it reduces auxiliary equipment, site preparation or downtime exposure.
Document the trade-off behind the selected option
The technical bid evaluation should record compliant points, deviations, assumptions and the reason for the recommendation. Keep commercial adjustments separate from technical ranking until the scope is aligned. This gives the project team a traceable basis for approval and later change management.
Keep a usable project record
Maintain one controlled file containing the approved duty sheet, supplier clarifications, drawings, component data, inspection records, test results, deviations, photographs and signed acceptance documents. Record document revisions and the person responsible for each open item. This prevents the operating team from receiving a package whose final configuration differs from the information used during procurement.
The handover set should also identify installed component models, consumables, calibration intervals, recommended spares, preservation requirements and supplier support contacts. Capture baseline operating readings when the unit is accepted. Those records give maintenance personnel a reference for condition changes and allow later modifications to be reviewed against the original design basis.
Before closing the project, confirm that operators can find the startup, normal-operation, controlled-shutdown and emergency procedures relevant to their unit. Training attendance alone is not sufficient; the responsible team should demonstrate the required checks and know which conditions require escalation rather than continued operation.
Codes, standards and project requirements
Confirm the final specification and acceptance plan against the owner’s project standards, local jurisdiction and OSHA oil and gas extraction safety guidance. The applicable project documents govern whenever they are more specific.